| Brand Name: | WeSeW |
| Model Number: | SS-717 |
| MOQ: | 1 pc |
| Price: | Price Negotiation |
| Payment Terms: | T/T,Western Union |
| Supply Ability: | 10,000 pieces per month |
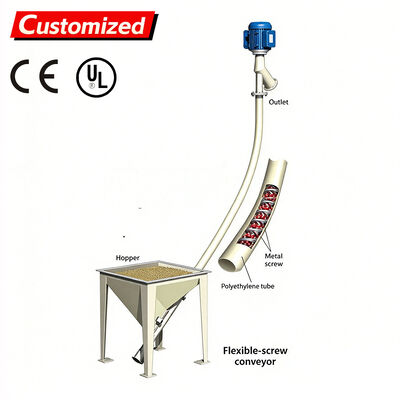
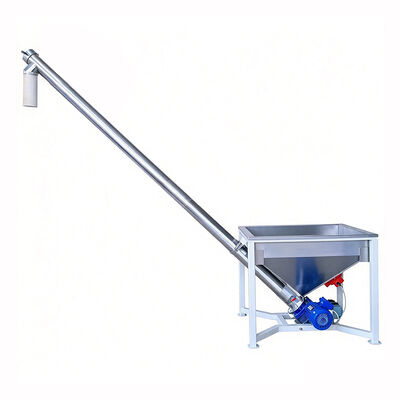
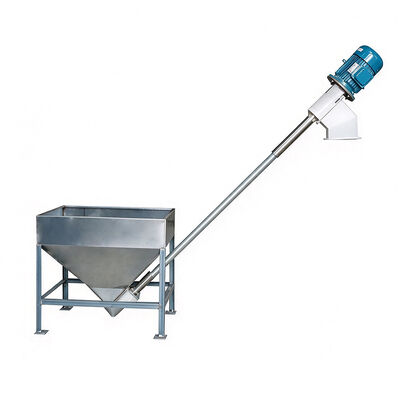
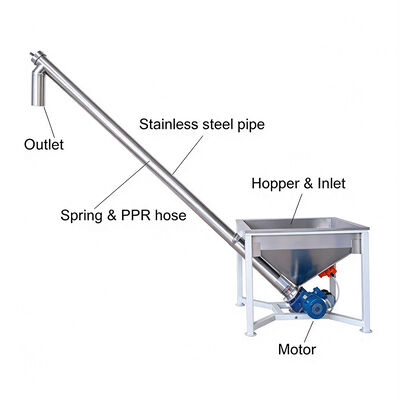
For industries that demand seamless, contamination-free, and low-maintenance transfer of dry bulk materials, our Flexible Screw Conveyor stands as the ultimate upgrade from traditional rigid conveying equipment. Engineered to eliminate the layout limitations, high operating costs, and material damage issues common to conventional conveyors, this system delivers consistent performance across food processing, pharmaceutical manufacturing, chemical production, plastic processing, construction material handling, and many other sectors. Unlike rigid screw conveyors, bucket elevators, vacuum conveyors, or drag chain systems, it combines fully enclosed transport, space-saving flexibility, and near-zero maintenance into one compact, easy-to-deploy unit that integrates perfectly into both new production lines and existing facility upgrades.
Every detail of our Flexible Screw Conveyor is designed to solve the most persistent pain points in daily material handling operations, bringing tangible improvements to your production efficiency and operational cost control.
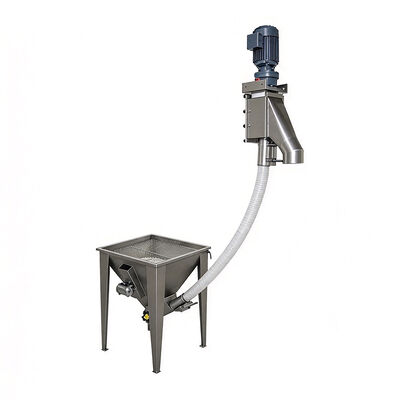
Breaking the restriction that traditional conveyors can only run horizontally or at a slight incline, our system supports free bending along your facility's existing structure, easily navigating around obstacles, equipment foundations, and limited-space work areas. It requires no dedicated large conveying corridor, making it the ideal choice for factories with tight floor space, multi-level processing lines, or frequent production layout adjustments. Even in narrow workshops where other conveying solutions cannot be installed, it can complete the material delivery path from the feeding point to the destination smoothly.
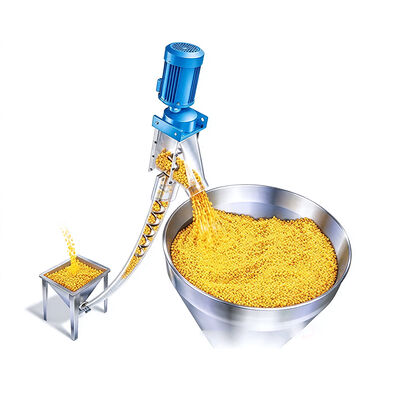
The rotating flexible screw pushes materials forward steadily inside the enclosed tube, without the high-speed impact, shear force, or material separation issues that often occur in pneumatic conveying or bucket elevator systems. This gentle conveying mechanism fully protects fragile granules, delicate food powders, precision pharmaceutical pellets, and special-shaped plastic particles, ensuring zero product breakage, no ingredient segregation, and consistent material quality throughout the entire transfer process.
One single unit can handle an extremely broad range of dry bulk materials, covering free-flowing and non-free-flowing powders, fine particles, small pellets, flaky materials, and even mixed bulk solids. Whether you are transporting cement, flour, sugar, chemical additives, plastic resin pellets, food grains, or pharmaceutical raw materials, this conveyor maintains stable and continuous delivery without jamming, material residue, or blockage, eliminating the need to replace different conveying equipment for different materials.
The entire system removes belts, chains, intermediate bearings, and other vulnerable moving parts completely. The only core moving component is the flexible spiral body running inside the sealed conveying tube, which avoids wear failure, part replacement, and the risk of lubricant leaking to contaminate materials. There is no daily lubrication, regular tension adjustment, or frequent component inspection work required, drastically cutting long-term maintenance costs and reducing unplanned downtime to the greatest extent.
Designed with a fully dismountable structure, one operator can complete the full disassembly of the conveying tube and spiral body in just 3 to 5 minutes, with no dead corners left for material residue. This design fully meets the strict hygiene standards of food processing and pharmaceutical production, supporting thorough cleaning, high-temperature disinfection, and cross-contamination prevention requirements between different batches of products.
With a simple direct-drive structure, the system does not require extra air supply systems, multiple sets of driving motors, or high-power vacuum generators. It runs with extremely low power consumption, helping you cut long-term electricity bills and reduce the comprehensive energy cost per ton of material conveyed.
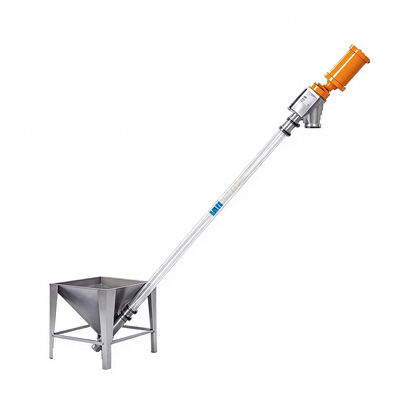
We provide fully customized services covering conveying length, tube material (food-grade hose, industrial anti-corrosion steel tube), screw material, feeding hopper design, mobile casters, and intelligent control modules. No matter your site requires horizontal conveying, vertical lifting, multi-point feeding, or multi-directional discharging, we can adjust the configuration to perfectly match your existing production line layout, with no extra large-scale facility transformation needed.
Our Flexible Screw Conveyor is not just a conveying device — it is a long-term cost-saving and efficiency-boosting solution built for your bulk material handling workflow.